Shenzhen Simpsons Refrigeration Technology Co., Ltd.


In the global industrial temperature control field, we are pragmatic and innovative pioneers, providing energy-saving and innovative solutions for global industrial development, which is our ideal pursuit of hard work.
Focusing on the field of industrial temperature control, let China's energy-saving solutions nourish the world
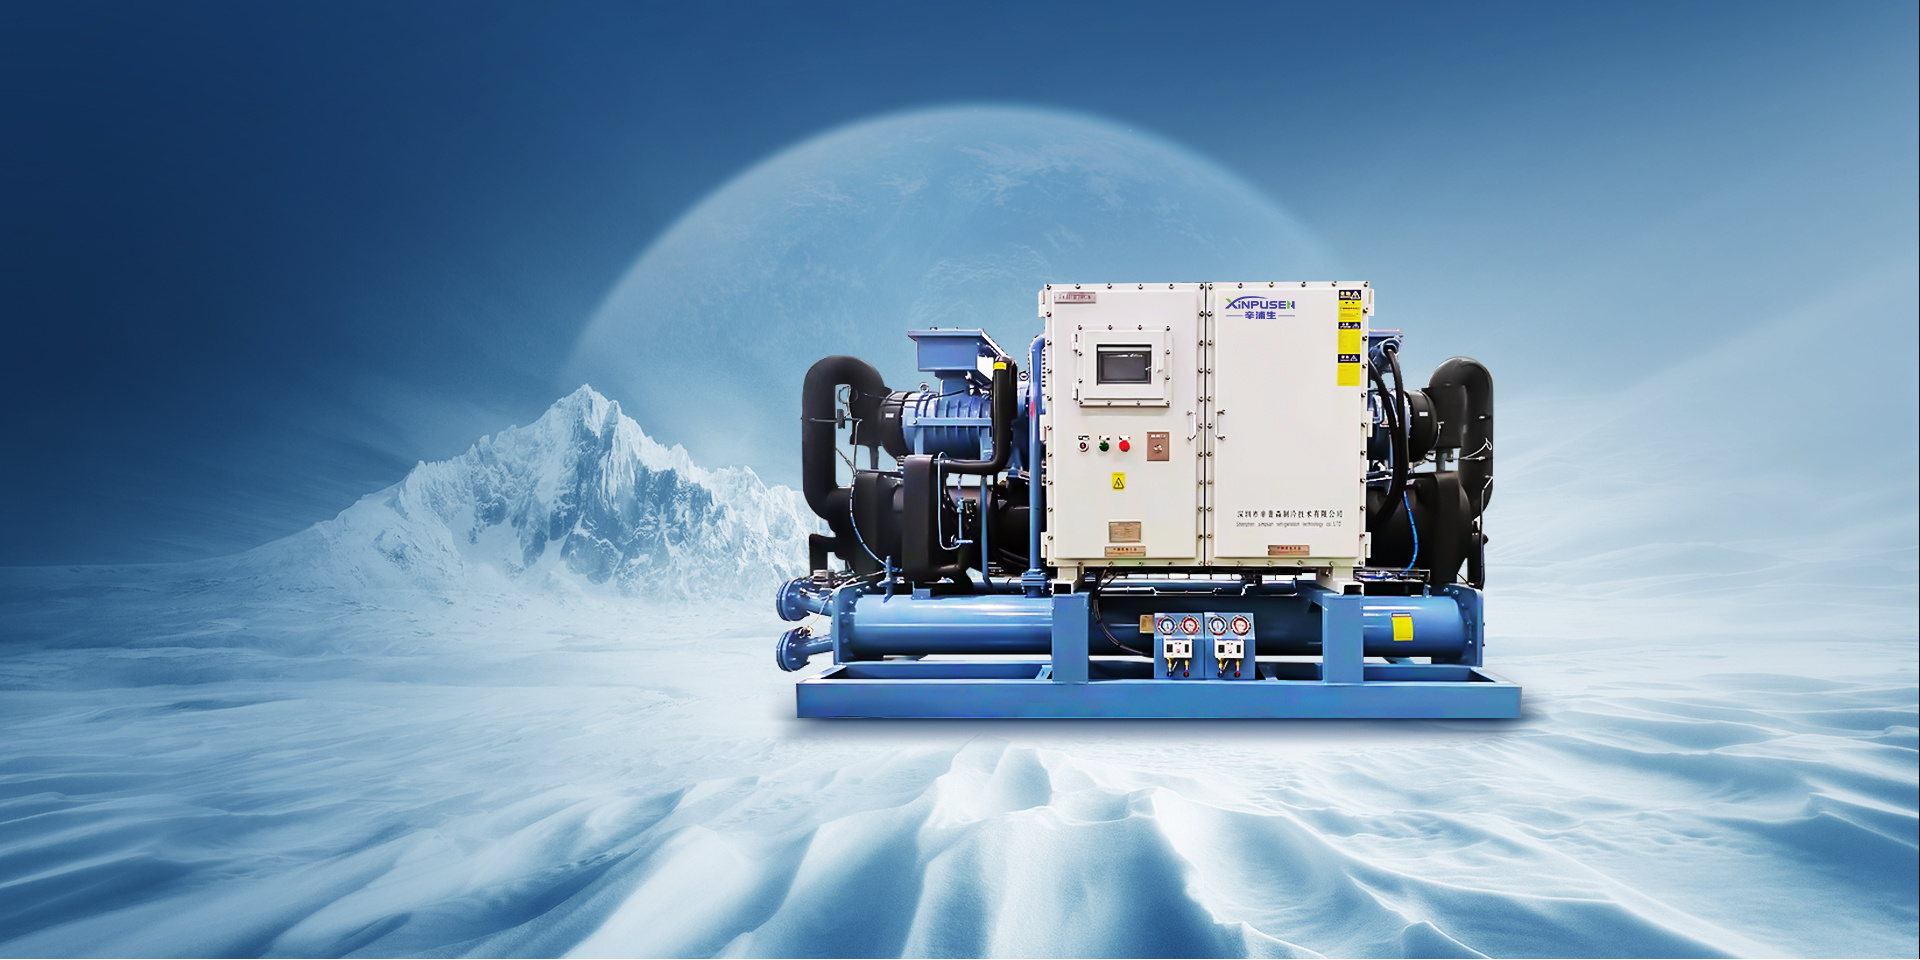
For products, we are seekers of perfection and excellence
Follow Simpson for the latest news
If you have any needs or suggestions, please contact us
 CN
 EN
Product Center
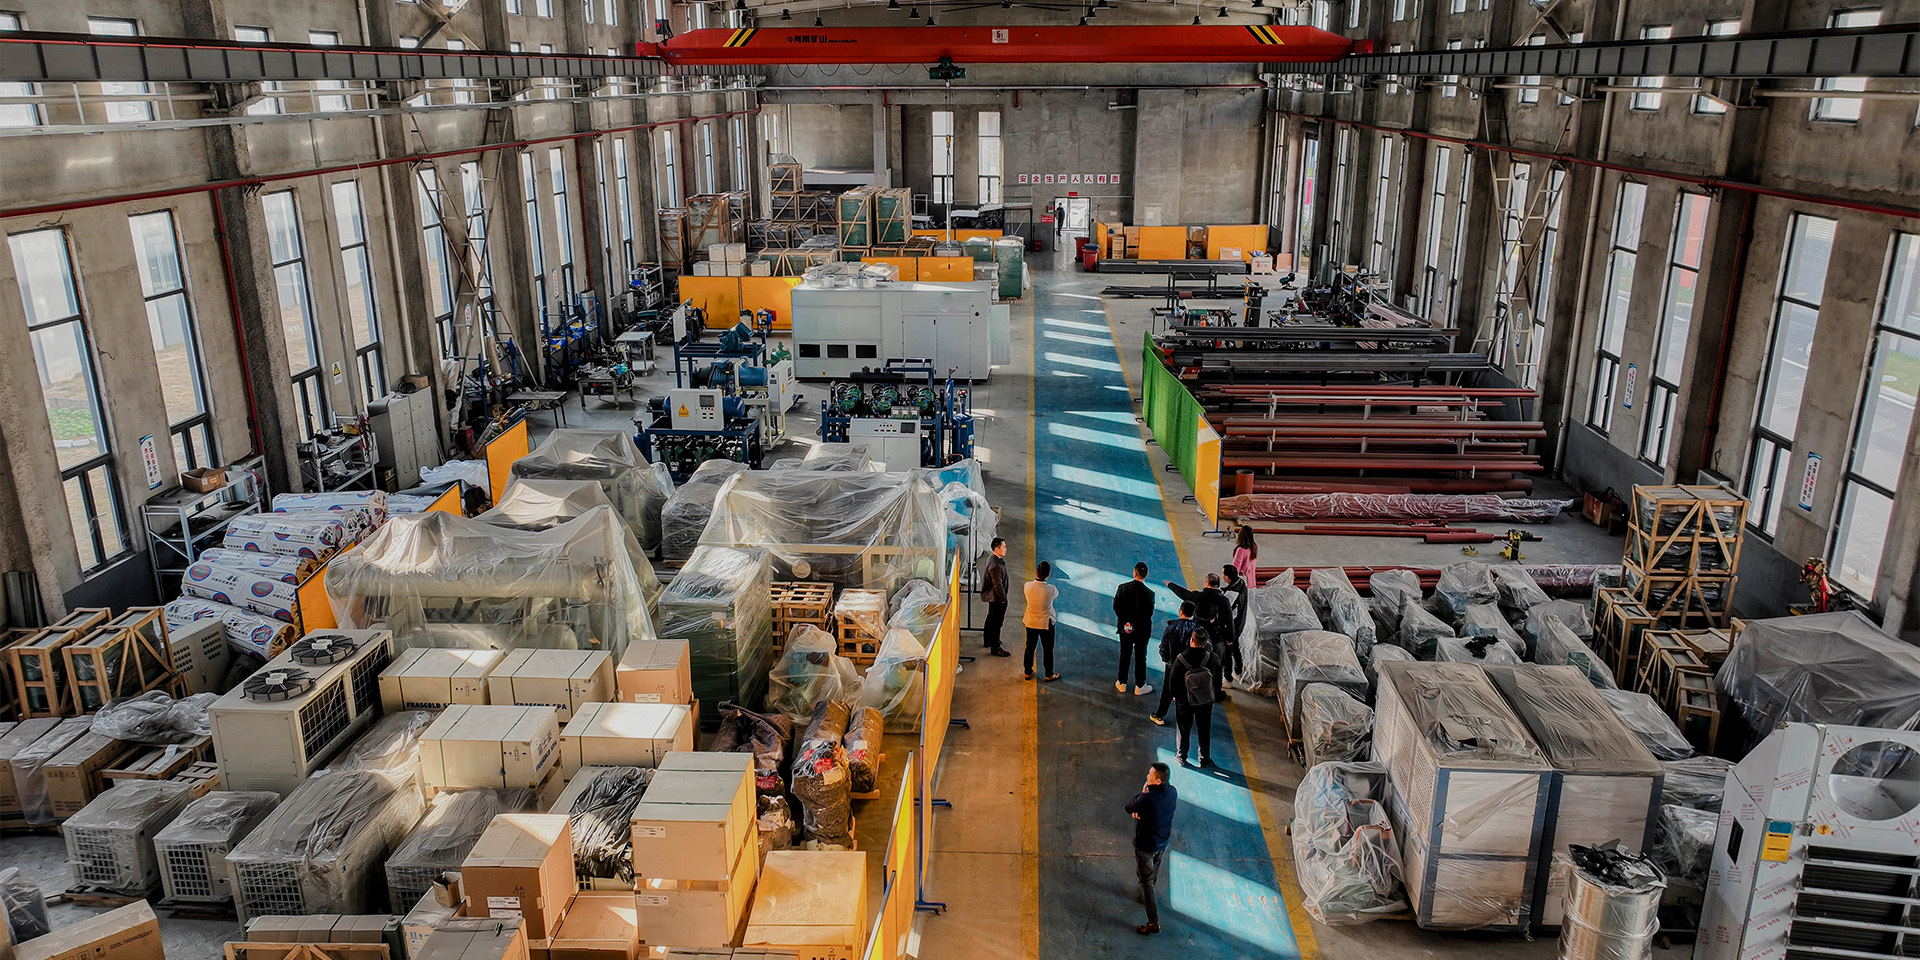
An international innovative enterprise specializing in industrial temperature control and refrigeration technology, integrating product research and development, production, sales, and service

High-Temperature Screw-Type Water-Source Heat Pump Unit
The Simpson high-temperature screw‑type water‑source heat pump unit is equipped with a screw compressor specially designed for high temperatures and uses the environmentally friendly refrigerant R134a. It efficiently recovers low‑grade waste heat from industrial wastewater, geothermal tailwater, and other sources, reliably producing high‑temperature hot water at 55°C to 90°C. The heating capacity ranges from 100 kW to 2100 kW, and the units support parallel expansion. Featuring precise temperature control and stable operation, they can be customized with variable frequency drives, explosion‑proof designs, or corrosion resistance, and are compatible with multiple industrial communication protocols for integration into smart control systems. They are widely applicable to clean heating applications such as industrial process hot water, centralized campus heating, and waste heat recovery across various industries.
Category:
Products
Special Customized Series
Product Attachment:
Product Introduction
- Heating capacity range: 100 kW to 2100 kW
- Temperature control range: 55°C~90°C
- Temperature control accuracy: ±1°C
- Refrigerant options: R134a, R515B
- Installation environment: indoor installation
- Customization options: explosion-proof, energy-saving variable-frequency, and corrosion-resistant heat exchanger customization
- Remote communication: MODBUS RTU RS485 optional or
- PROFINET Industrial Ethernet Communication Interface
Product Features
- Equipped with a high-temperature-specific semi-hermetic twin-screw compressor, it is optimized for high-temperature applications with large compression ratios, delivering high heating efficiency and smooth operation. Standard features include stepless capacity modulation from 25% to 100%, with optional inverter drive, enabling demand‑based matching of thermal load and significantly enhancing energy savings under varying operating conditions.
- It employs a high-efficiency enhanced shell-and-tube heat exchanger and an optimized media distribution structure, delivering high heat transfer efficiency and small temperature differentials. It is adaptable to complex waste heat conditions, precisely maintaining a constant outlet water temperature within ±1°C, and ensuring excellent heating stability.
- A dedicated, high-efficiency oil separation and return system is configured to suit high-temperature, high-pressure operating conditions, effectively preventing oil accumulation in the heat exchanger that would degrade heat transfer performance, thereby ensuring 24-hour continuous and stable unit operation with lower O&M costs.
- Industrial-grade, fully optimized system design ensures wide-condition adaptability to various low-temperature waste heat sources. It replaces conventional boilers for heating, offering zero emissions, low energy consumption, and high safety, while demonstrating strong resistance to load fluctuations and water quality variations, making it suitable for a range of complex industrial settings.
- Equipped with an intelligent PLC control system, it features fully automatic load regulation, integrates multiple safety protection mechanisms, and supports self-diagnosis of faults, remote monitoring, and interlocked control, ensuring the unit operates safely and efficiently across all operating conditions.
Keyword:
Previous Page
Next Page
Previous Page
Next Page
More Products


Inquire Now
If you are interested in our products, please leave your email address, and we will contact you as soon as possible, thank you!
Subscribe to our instant updates
Providing energy-efficient and innovative solutions for global industrial development


Marketing Center: Building K, No.1 Xiawei Industrial Zone, Zhangxi Community, Guanhu Subdistrict, Longhua District, Shenzhen
Production Base: Building 1, Yongsheng Science and Technology Industrial Park, No.26 South Shahu Xinyuan Road, Tangxia Town, Dongguan
0755-21017010
189-2749-0225
0755-23771793
Scan to add WeChat
© COPYRIGHT 2024 Shenzhen Xinpusen Refrigeration Technology Co., Ltd. ALL RIGHTS RESERVED Powered by www.300.cn